
pharma-packaging

Fill out the form below with your packaging requirements, dimensions, quantity, and artwork files. I will review everything and get back to you with the best quote.
We found 5 items for you!


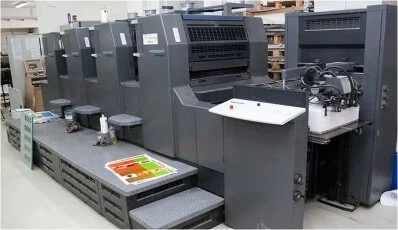
Offset printing is a high-volume printing technique using metal plates and rubber blankets.
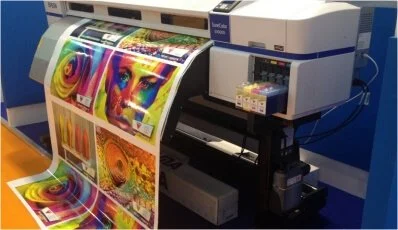
Digital printing is a method of printing directly from digital files to media.
UV printing uses UV light to instantly cure ink onto a wide variety of materials.
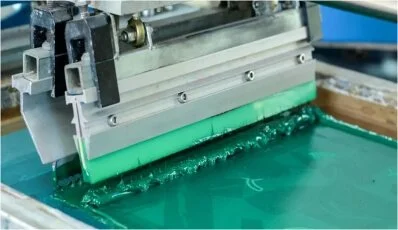
It is a process that transfers ink through a stenciled mesh screen onto a surface.
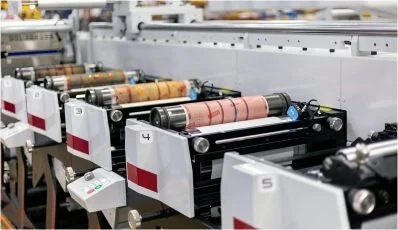
Flexography is a high-speed printing process using flexible plates and low-viscosity inks.
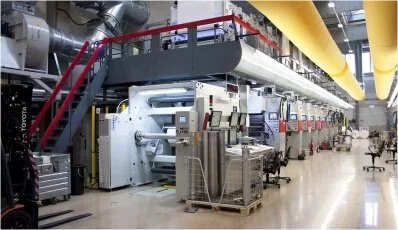
Gravure printing is a high-quality, high-speed intaglio printing method using engraved cylinders.

This method applies heat to bond glittering metallic hues like gold or silver onto paper, creating designs that truly shimmer.

This approach raises the paper from below to form a tactile image you can feel with your fingertips.
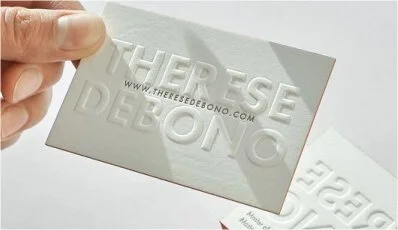
This technique indents your design into the paper, producing a striking recessed effect that brings dimension to your work.

This unique foil shifts through a vibrant spectrum of colors like a dazzling rainbow when light strikes it at specific angles.

This glossy clear varnish targets select areas of the page to highlight particular elements with eye-catching shine.

This sleek coating delivers a non-reflective, velvety texture that feels luxurious and enhances readability.
This highly reflective layer bounces back light, amplifying colors to make your print vibrant and dynamic.
Hot foil stamping is a printing method using heat to transfer foils for decoration.
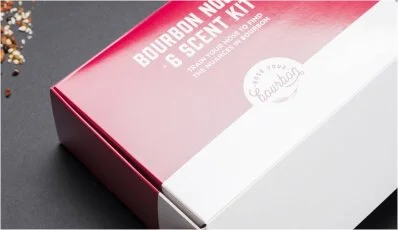
A quick-drying, water-based layer that shields paper from smudges and grime while being eco-friendly.
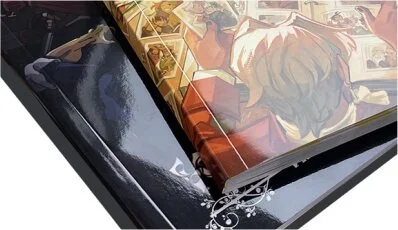
This liquid finish cures under UV lights, giving your paper a vibrant, glossy shine.

This glossy treatment applies only to select areas, making images or text dramatically stand out.
This unique finish creates a velvety or suede-like texture under your fingertips.
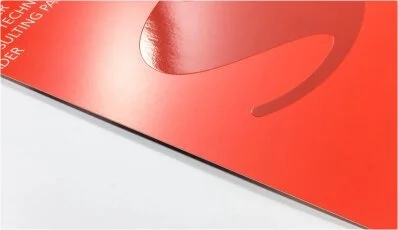
A transparent ink that safeguards the page or provides subtle gloss, though it may yellow with age.
A thin plastic film bonded to paper for durability, available in shiny or non-glare finishes.
A rugged plastic barrier that stops scratches and wear from frequent handling.
This layer delivers a luxurious smooth feel and exceptional tear resistance.
Premium solid bleached sulfate, C1S coated for vibrant prints and superior food safety.

Solid bleached sulfate, double-coated for flawless printing and premium packaging appeal.
Pure uncoated unbleached kraft ensures raw, sustainable strength for authentic eco-packaging needs.

Clay-coated newsboard delivers affordable strength with smooth surface for bold branding.

Bold black kraft exudes premium elegance and robust protection for standout packaging.
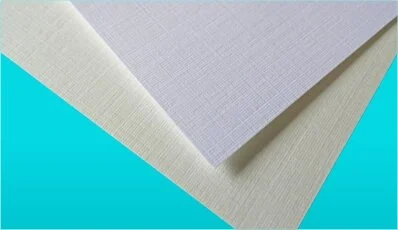
100% recycled clay-coated newsboard offers eco-friendly durability and cost-effective packaging solutions.
Rustic natural brown kraft provides authentic, biodegradable strength for sustainable food packaging.
Clean white kraft combines natural strength with bright, recyclable appeal for branding.
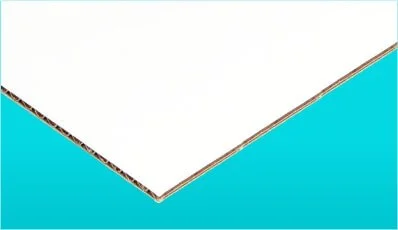
Rugged natural kraft corrugated board delivers eco-friendly strength for reliable food transport.
Elegant oyster white corrugated board offers subtle sophistication and sturdy packaging protection.
Smooth kemi white corrugated ensures crisp prints and robust durability for premium shipping.
Bright bleached white corrugated provides pristine appearance with superior strength for branding.
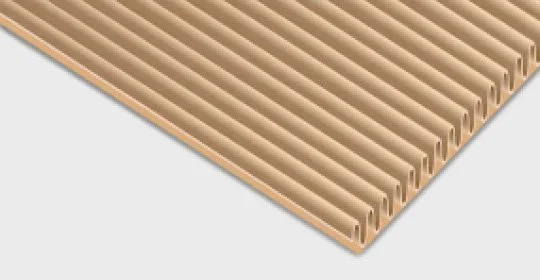
Tall A-flute excels in superior cushioning and shock absorption for fragile foods.
Fine B-flute offers smooth printing surface and efficient collapse resistance for boxes.
Versatile C-flute balances strength, printability, and space efficiency for standard packaging.
Micro E-flute creates sleek, flat profiles with excellent print quality for retail.
Single face flute adds lightweight protection and flexibility for delicate food wrapping needs.
Single wall corrugated flute balances cost and cushioning for everyday food shipping demands.
Double wall flute delivers enhanced stacking strength for heavier food packaging loads.
Triple wall flute provides maximum crush resistance for industrial food transport durability.

It is a type of paperboard with a white clay-coated top side, ideal for luxury packaging.

Grey Chipboard Cardboard is a thick, sturdy material made from recycled content, ideal for luxury packaging.
This material is slim yet robust enough to maintain its form effectively for petite, lightweight boxes and resilient cards.
An excellent balanced option that offers a firm feel and reliable safeguarding for typical gift box varieties.
This dense board has a substantial heft in your grasp and ranks as the top pick for superior, long-lasting luxury packaging.
This exceptionally sturdy and inflexible material suits bigger items requiring additional reinforcement for security.
The densest and most resilient choice on offer, giving it a near-wooden sensation for the ultimate premium goods.
Can’t find what you are looking for? Fill out our quotation form, and our team will design a custom box solution that fits your product perfectly.
Pharma boxes are specially designed packaging solutions used to pack, protect, store, and present medical products. These include tablets, capsules, syrups, ointments, injections, and many other healthcare items. Unlike regular retail packaging, pharmaceutical boxes must follow strict safety, hygiene, and regulatory standards. Their main purpose is not only to hold the product but also to maintain its quality during storage, shipping, and shelf display.
In today’s competitive healthcare market, brands focus on well structured pharma packaging that ensures both protection and clear communication. Information such as dosage, ingredients, expiry date, and usage instructions is printed on these boxes, making them essential for safe consumption.
The importance of pharmaceutical boxes goes far beyond simple packaging. They help build trust between healthcare providers and consumers. A well designed pharmaceutical product packaging system ensures medicines reach patients in safe condition. Even slight damage or contamination can reduce product effectiveness.
Many manufacturers invest in custom pharma boxes to improve brand recognition and patient confidence. Secure packaging reduces risks of tampering and supports compliance with global regulations. Reliable drug packaging boxes also simplify handling for pharmacies, hospitals, and distributors.
There are various packaging styles depending on product form and market needs. For example, tablet packaging boxes and capsule packaging boxes are commonly used for solid dose medicines. Liquid medicines often use cartons that hold bottles securely.
Retail pharmacies often require retail medicine boxes that allow quick identification and organized shelf placement. Over the counter medicines use OTC medicine packaging with attractive graphics to catch consumer attention. In addition, bulk shipments may use mailer boxes to ensure safe transport between warehouses and clinics.
Material selection plays a key role in packaging performance. Many companies prefer pharmaceutical carton packaging made from high quality paperboard. This material is lightweight yet strong, making it suitable for automated packing lines.
Common paperboard options include SBS board, kraft paperboard, and corrugated stock. Durable pharmaceutical paper boxes offer good print quality and structural integrity. For eco conscious brands, recyclable board is a growing preference.
Some packaging requires extra strength, especially when transporting fragile vials or heavy medical kits. In such cases, sturdy cardboard boxes or layered corrugated structures provide the needed support. Brands that want a natural look often choose kraft boxes, which also appeal to sustainability focused customers.
Safety is always the top priority in healthcare packaging. Features like tamper evident seals, moisture resistance, and child resistant locks are now common in protective medicine packaging. These elements help maintain product stability and reduce misuse.
Another important feature is precise die cutting. Custom shaped inserts and partitions, often made using Die Cut Boxes, keep medicines fixed inside the carton. This reduces movement during shipping and prevents damage.
Many companies also use barcodes and QR codes in pharmacy packaging boxes to improve traceability. These technologies support inventory management and ensure authenticity verification.
Printing is not only about design but also about communication. Clear typography and color coding improve readability and reduce dispensing errors. High resolution pharma box printing helps display essential details such as manufacturing information and warnings.
Healthcare brands rely on printed pharma boxes and custom printed medicine boxes to stand out on crowded shelves. Attractive graphics combined with compliance information create balanced packaging that is both functional and appealing.
Leading manufacturers like The CardBoard Boxes understand that branding should never compromise safety. Their approach combines creative layouts with strict quality control, ensuring packaging meets both marketing and regulatory needs.
Every country has guidelines for prescription packaging and labeling. Packaging must include clear instructions, batch numbers, and expiry dates. Well structured medicine packaging boxes support these requirements and help avoid legal complications.
For sensitive drugs, packaging must protect against light, humidity, and temperature fluctuations. Multi layer board and coated surfaces improve resistance. Reliable medical packaging boxes also help maintain sterility during transportation.
Compliance is not limited to printing. Structural testing, stacking strength evaluation, and drop tests are part of modern packaging development. Companies invest in pharma product boxes that pass these checks and maintain consistent performance across supply chains.
Folding cartons remain the most popular choice due to their cost effectiveness and versatility. Folding carton pharma boxes are easy to assemble and suitable for mass production. Sleeve cartons, tuck end boxes, and crash lock bases are widely used formats.
For promotional campaigns or new product launches, brands use countertop display boxes to improve visibility. These boxes allow pharmacists and retailers to present medicines neatly while saving shelf space.
Premium treatments or supplements may use rigid or magnetic closure packaging for a high end feel. Even in pharmaceutical markets, packaging aesthetics can influence buying decisions.
Selecting the right packaging depends on several factors such as product size, fragility, storage conditions, and distribution method. Manufacturers often start by defining whether they need healthcare packaging for retail shelves or bulk transit.
If the medicine is sensitive to moisture, coated boards or laminated cartons may be required. For high volume logistics, reinforced pharmaceutical box manufacturer solutions can reduce shipping damage and returns.
Customer demand is also evolving. Many healthcare brands now request sustainable materials, easy open features, and compact designs. Partnering with experienced providers like TheCardBoardBoxes helps businesses balance innovation, compliance, and cost efficiency.
Packaging acts as the silent ambassador of a pharmaceutical brand. Clean layouts, informative content, and sturdy structure create confidence among buyers. Effective branded pharma packaging improves recall and builds long term loyalty.
Well designed boxes also simplify the work of pharmacists and medical staff. Organized packaging systems improve dispensing speed and reduce confusion. Whether it is small clinics or large hospitals, dependable pharma packaging solutions play a crucial role in daily operations.
In the end, pharma boxes are more than containers. They are protective systems, communication tools, and marketing assets combined into one. With growing competition and strict safety expectations, investing in smart pharmaceutical packaging is no longer optional. It is essential for sustainable growth in the healthcare industry.
All the relevant questions about custom boxes and packaging have been answered. If you still have any other questions, contact us anytime by phone, chat, or via the contact form.